
Saltwater creates an electrolyte that accelerates corrosion when moisture reaches exposed conductive metal. As corrosion moves along bare copper strands or beneath insulation, it can reduce usable cross-section and increase electrical resistance.
Tinning changes this behavior by coating each copper strand with a protective metal layer. The barrier delays direct exposure to saline moisture, which supports more stable conductor performance in wet environments.
For a tinned copper wire marine specification, conductor selection forms only one part of the construction strategy. Moisture can also enter through connector interfaces, cable entries, splices, and damaged jackets.
IPX ratings address controlled water exposure, while salt-spray testing compares corrosion resistance under defined laboratory conditions rather than guaranteeing a specific service life. Sealed terminations, suitable connectors, and voltage-drop calculations then connect these requirements to the complete harness.
Why Tinned Copper?
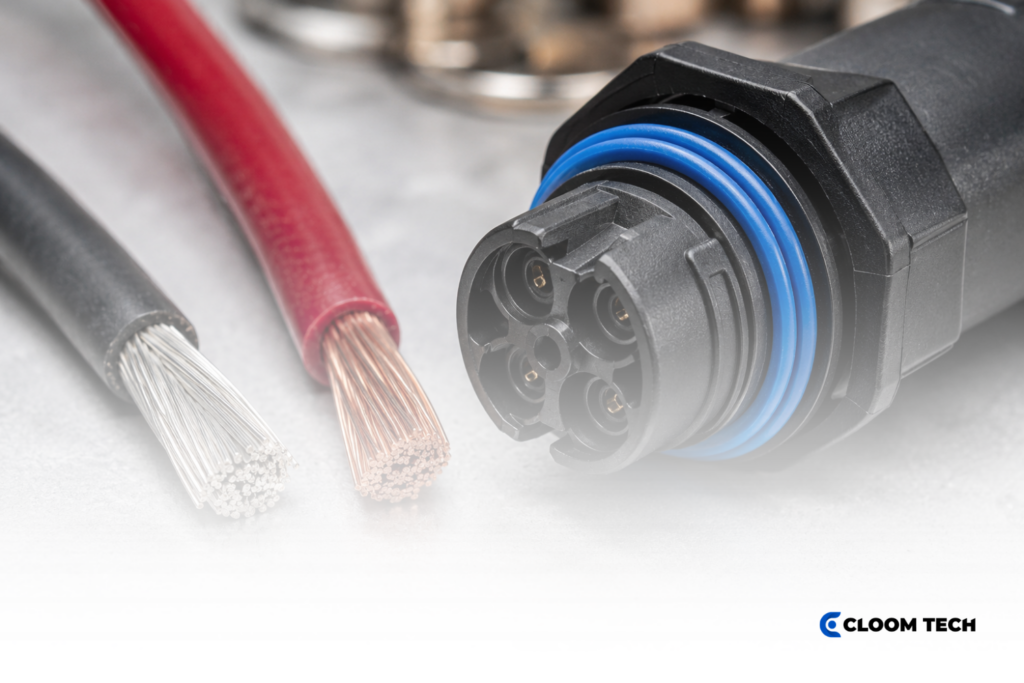
Tinned copper suits wet marine zones because its plated surface separates the copper substrate from direct contact with oxygen, moisture, and chlorides. Once bare copper becomes exposed, corrosion products can spread between strands and interfere with the conductor-to-terminal interface.
Tin does not make a conductor immune to corrosion. Instead, the coating delays direct exposure of the copper beneath it, allowing processing to leave the plating intact. Chlorides and oxygen can still attack the tin coating and copper substrate, particularly around damaged or highly stressed areas. Adhesive-lined seals also limit moisture migration from the ends of exposed conductors.
This system-level view matters when selecting tinned copper marine wire. Plating protects the strands, while termination sealing protects the freshly stripped end and limits capillary moisture movement.
The tin layer adds material and processing cost, while bare copper provides marginally higher initial conductivity. That small electrical advantage loses practical value if corrosion later reduces the conductor’s effective area or raises termination resistance.
| Comparison point | Tinned copper | Bare copper |
|---|---|---|
| Surface protection | Tin covers each strand and delays copper exposure | The copper surface remains directly exposed after moisture enters |
| Saline environments | Better suited to bilges, decks and other wet zones | Best limited to locations that are demonstrably dry and protected. |
| Terminations | Plating supports corrosion-resistant crimp systems | Exposed ends need effective moisture control |
| Electrical behavior | Slight conductivity trade-off with more stable long-term protection | Highest initial conductivity with greater corrosion sensitivity |
| Cost | Higher initial material cost | Lower initial material cost |
IPX Ratings, Decoded by Boat Zone
IPX ratings describe an enclosure’s performance in specific water tests, not a universal guarantee that an installed harness will remain dry. IP codes separate solid-particle protection from water protection. An X means the product does not declare a solid rating in that position.
| Boat zone | Relevant water exposure | Practical rating starting point | Specification focus |
|---|---|---|---|
| Cabin interior | Condensation or occasional drips | IPX4, where splash exposure remains possible | Cable entries, ventilation, and leak paths |
| Exposed deck | Rain, spray, and washdown jets | IPX6 | Jet direction, connector orientation, and capped unmated interfaces |
| Engine bay | Spray, condensation, heat, and vibration | IPX6 or IPX7, depending on mounting | Seal materials, strain relief, and temperature compatibility |
| Bilge | Temporary or sustained immersion | IPX7 or IPX8, depending on duty | Complete mated assembly, splice sealing, and cable-end migration |
IPX6 tests resistance to powerful water jets, while IPX7 tests resistance to temporary immersion under defined conditions. IPX8 addresses continuous immersion under conditions agreed between the manufacturer and user, so the marking needs a stated depth and duration.
These ratings apply to the tested configuration. A connector carrying an IPX8 label may still form part of a vulnerable system if an open backshell, splice, or jacket breach creates another path. Mating condition also matters because some interfaces achieve their rating only when fully coupled and locked.
Zone selection begins with credible exposure, then adds routing, drainage, and maintenance access. A deck connector may need jet protection without immersion capability, whereas a low-bilge branch needs an assembly-level immersion strategy.
What Salt-Spray Testing Really Proves
Salt-spray testing checks how specified materials, platings, and protective finishes respond inside a controlled corrosive atmosphere. A salt-spray apparatus uses standardized operating conditions, whereas neutral and accelerated procedures require defined equipment and reagents.
Test Conditions Behind the Hours
A test plan sets the specimen condition, exposure method, duration, and acceptance criteria. The report should identify the standard edition, solution, temperature, sample preparation, evaluation points, and any post-test electrical checks. Without those details, an hours figure offers little basis for comparison.
Why Hours Do Not Equal Service Life
Salt-spray procedures do not assign a universal exposure period or interpretation to every product. The results also cannot rank unrelated materials or predict long-term corrosion resistance. A 1,000-hour result doesn’t equal a defined number of years at sea.
Hours become useful when two options follow the same method, specimen preparation, and acceptance criteria. Even then, the result compares performance within that test program rather than forecasting field life. Real vessels are exposed to ultraviolet light, vibration, wet-dry cycles, temperature changes, contaminants, and mechanical damage.
Electrical Checks Beyond Visible Corrosion
Visible corrosion provides only one evaluation point. Testing marine tinned copper wire may also include continuity, insulation resistance, contact resistance, and seal-integrity measurements. Those checks reveal an electrical change that appearance alone could miss.
Marine Harness Construction Essentials
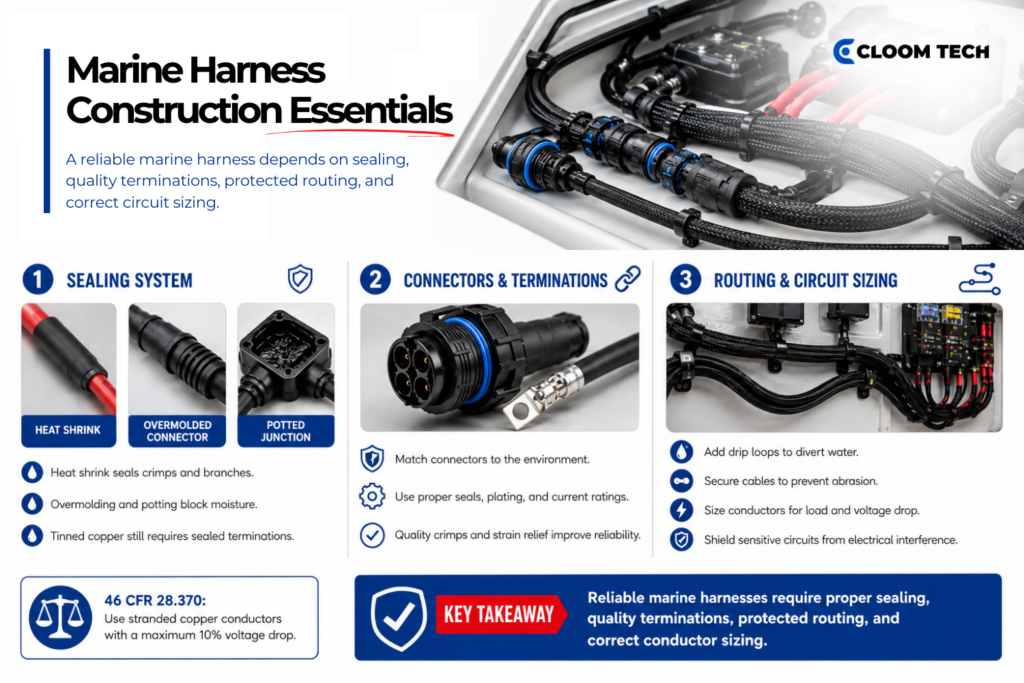
Marine harness construction combines corrosion-resistant conductors with sealing, suitable interfaces, and circuit sizing. One strong component cannot compensate for an exposed splice, unsupported branch, or undersized return path.
Sealing Methods Work as a System
Adhesive-lined heat shrink can seal crimp barrels and branch transitions when the adhesive bonds continuously to compatible insulation. Overmolding provides a repeatable barrier around selected connector-to-cable transitions, while potting can protect fixed junctions with limited service access. Each method needs compatible materials, controlled processing, and inspection criteria.
A harness built with tinned copper marine wire still depends on these barriers since the stripped ends expose the conductor beneath the plating.
Connectors and Termination Quality
Connector selection starts with the installed zone rather than an IP label alone. Housing materials, seals, terminal plating, current capacity, and mating cycles must match the circuit and environment. Strain relief should transfer movement to the cable jacket rather than the conductor termination. Service loops and accessible locking features then support later inspection.
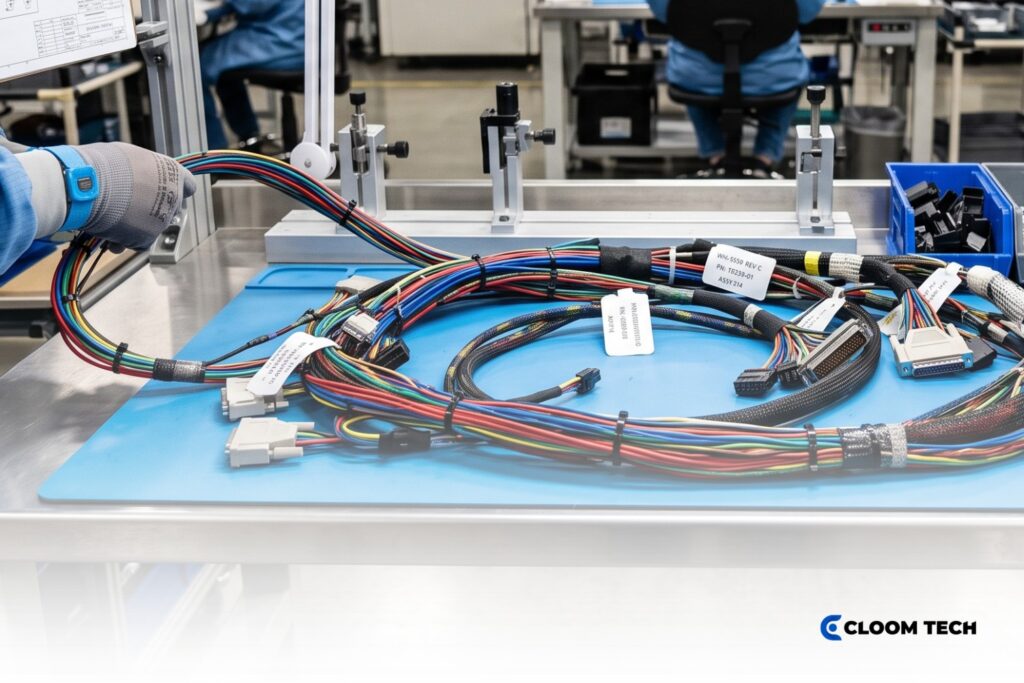
Terminal processing deserves equal attention because an incorrect strip length or crimp can expose copper and weaken mechanical retention. Documented tooling, pull testing, and visual criteria make termination quality measurable across production batches.
Routing and Circuit Sizing
Routing also protects the sealing system. Drip loops direct water away from entries, supported runs limit abrasion, and downward-facing interfaces reduce pooling. Deck and engine-bay routes may also need ultraviolet, oil, fuel, or temperature resistance beyond water protection.
Conductor size must satisfy ampacity and voltage drop requirements along the entire current path. The calculation needs the installed circuit topology, route length, and operating load. For covered commercial fishing vessels, 46 CFR 28.370 requires stranded copper conductors sized for the circuit and limits load-terminal voltage drop to 10%.
Different vessel categories and circuit functions may require tighter limits. Starting current, continuous load, bundling, ambient temperature, and terminal losses also affect the final size. Sensitive marine electronics may also require harness shielding when nearby motors, alternators, or transmitters threaten signal quality.
Specifying a Marine Harness (Checklist)
A complete request for quotation links each circuit to its electrical load, physical route, and environmental zone. That information lets a manufacturer quote materials, sealing processes and verification work against the same baseline.
For marine tinned copper wire, the request should specify the strand construction, insulation, and conductor coating. This detail prevents material assumptions from changing the harness response to movement, heat, or installation constraints.
Include these specification points:
- Electrical schedule: State nominal voltage, continuous current, starting or surge current, and allowable voltage drop for every circuit.
- Route definition: Give the complete supply-and-return length, branch locations, bend constraints, support points, and available installation space.
- Environmental zones: Identify cabin, deck, engine bay, and bilge sections, including expected immersion, washdown, chemical exposure, heat, and ultraviolet exposure.
- Conductor requirements: Specify tinned copper, stranding, insulation, temperature rating, color identification, and applicable cable standards.
- Connector interfaces: List part numbers, pinouts, mating equipment, keying, plating, current rating, and required mated or unmated protection.
- Sealing requirements: Define IPX targets, immersion depth and duration, heat-shrink locations, overmolding, potting, and permitted splice methods.
- Mechanical protection: Record vibration, abrasion, strain-relief, sleeving, clipping, and bulkhead-entry requirements.
- Verification plan: Name the salt-spray method, exposure hours, acceptance criteria, electrical tests, sample quantity, and documentation package.
- Production information: Provide pre-existing drawings, bill of materials, prototype quantity, production volume, and approval stages.
- Serviceability details: Define labels, connector access, replaceable sections, inspection points, and diagnostic breakouts.
The RFQ should distinguish mandatory requirements from preferences. It should also identify who approves substitutions, test deviations, and drawing changes before production begins.
What Should Go Into a Marine Harness RFQ So Vendors can Quote Accurately?
An accurate RFQ needs drawings, circuit loads, complete route lengths, environmental zones, volumes, and required test evidence. Buyers often omit immersion depth, unmated connector exposure, allowable voltage drop, or salt-spray acceptance criteria.
The request should also identify service-life expectations as application goals rather than guaranteed outcomes. Approval responsibilities for material substitutions, drawing revisions, and test exceptions help vendors price the same defined scope.
Cloom Tech manufactures custom marine wire harnesses and cable assemblies for wet, saline, and vibration-prone environments. Our ISO 9001, TS16949, IATF 16949, and IPC/WHMA-A-620 credentials support controlled production and harness-specific quality requirements.
With manufacturing in China and the Philippines, we combine global material sourcing with internal and third-party inspections. Share your pre-existing drawings, environmental zones, circuit loads, sealing targets, and testing requirements. Our team can provide Design for Manufacturability (DFM) feedback and recommend suitable material or production changes without assuming full design responsibility.
Contact us to discuss your marine harness specification.
Marine Wire Harness Construction FAQs
Can I mix tinned and bare copper in the same marine wiring system?
Yes, tinned and bare copper can coexist when each run suits its exposure and every transition uses a compatible termination. The conductor coatings alone do not create the primary galvanic concern because the connection system controls metal contact and moisture entry.
Mixed use makes the most sense when bare copper is kept in a genuinely dry, sealed area. Tinned copper should be used on wet or salt-prone routes. Clear documentation also prevents a future technician from assuming every conductor has the same corrosion protection.
Does every circuit on a boat need tinned copper, or only certain runs?
Not every circuit needs identical corrosion protection, although tinned copper provides a sensible default for exposed marine routes. Bilge, deck, and engine-bay circuits receive the strongest justification because they are subject to immersion, spray, condensation, or chemical contamination.
A dry cabin circuit may present lower exposure. Access difficulty and failure consequences can still justify the material premium, particularly when later replacement would require extensive disassembly.
Are IPX ratings, on their own, enough to guarantee a leak-free harness?
No, an IPX rating cannot guarantee that the complete harness will remain leak-free. Use it as one acceptance requirement within the broader harness specification.
State the mating condition, complete test configuration, exposure level, and post-test checks. Assembly-level verification then shows whether the connector, cable entries and sealed branches meet the same water-ingress target together.
How should I read “hours” claims in salt-spray tests when comparing harness options?
Treat 500-hour and 1,000-hour claims as relative screening indicators only when both options follow the same test plan. Neither figure represents a service-life promise.
Ask what counted as failure because visible corrosion, contact-resistance drift, and seal leakage measure different outcomes. The complete report matters more than the headline number.
What’s the biggest mistake specifiers make with marine harness voltage drop?
The most common mistake is calculating only the one-way route. Current travels through the supply and return path, so both lengths contribute to resistance and voltage loss.
Specifiers should also include starting current, connector losses, and shared return conductors. A wire size that works for steady operation may produce excessive drop during motor startup or peak equipment demand.
Can a general-purpose industrial harness be “upgraded” for marine use, or should it be redesigned?
An industrial harness can sometimes be upgraded when its conductor material, insulation, and circuit sizing already meet the marine exposure requirements. Revised sealing, strain relief, jacketing, or connectors may then close specific gaps.
A fresh specification becomes more appropriate when moisture can reach bare conductors, branches lack serviceable sealing, or voltage drop exceeds the circuit limit. Extensive piecemeal changes can also make testing and configuration control harder to document.
How do marine harness specs affect long-term maintenance and troubleshooting?
Good specifications make faults easier to locate without disturbing sealed sections. Durable labels, accessible connectors, documented pinouts, and planned test points let technicians systematically isolate a circuit.
Replaceable branches can also limit the scope of repairs. At the same time, routing should keep inspection points accessible without placing connectors where water pools or mechanical damage becomes likely.
Back to Top: Marine Wire Harness Construction: Tinned Copper, IPX Ratings, and Salt-Spray Testing
