
Sourcing from a Chinese wire harness manufacturer before completing an evaluation process exposes the program to quality and cost risks. Although an acceptable prototype confirms one build, it doesn’t establish production repeatability.
That distinction becomes critical when crimp performance lacks documented evidence or component changes proceed without customer approval. If these issues emerge during volume production, containment and replacement shipments add cost. The program may face further delays if another supplier must qualify the assembly.
A harness-specific vetting checklist addresses this uncertainty before production approval. By replacing generic supplier questions with checks for workmanship controls and testing records, it creates a documented sourcing decision based on verified manufacturing capability.
The Vetting Checklist at a Glance
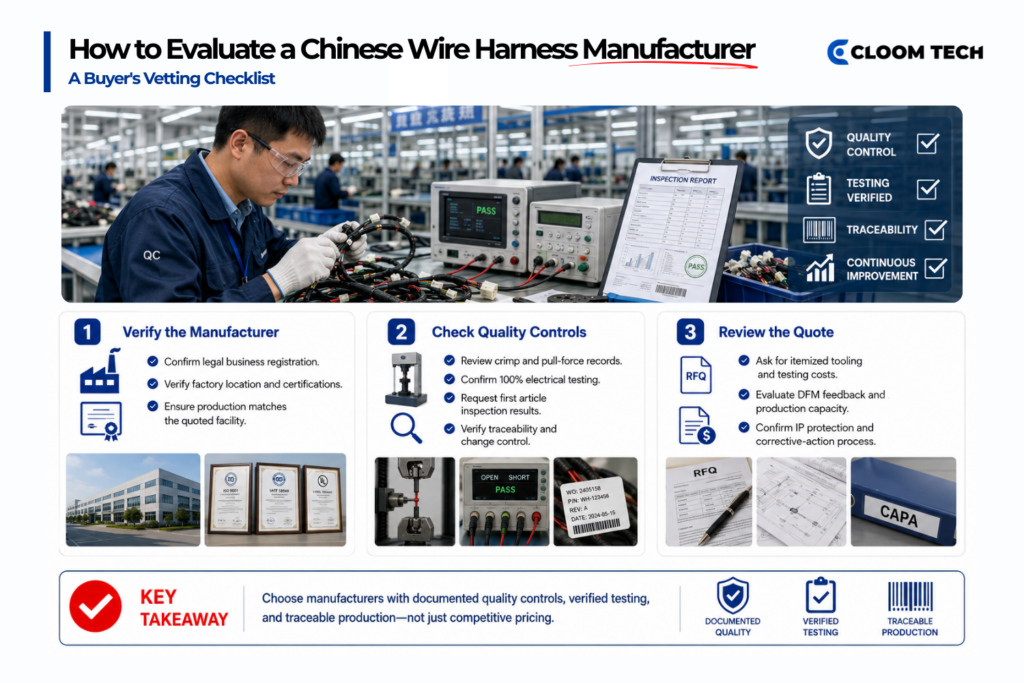
A wire harness supplier should demonstrate that the quoted factory performs the work and adheres to controlled workmanship standards. When determining how to choose a wire harness manufacturer, ask for the test records that link the approved sample to volume production.
Capacity records and material lead times should support the schedule proposed by each supplier identified through a wire harness manufacturer China search.
| Criterion | Evidence to Request | What Good Looks Like |
|---|---|---|
| Legal identity | Business license and Unified Social Credit Code | The registered entity matches the quotation and factory |
| Factory status | Audit report or live production tour | Equipment and records belong to the quoted operation |
| Certifications | Current certificates with a complete scope | The entity and site match the proposed manufacturing location |
| Crimp control | Pull-force results and crimp-height records | Measurements match approved terminal specifications |
| Electrical testing | Test plan and representative report | Every completed harness receives the specified checks |
| First article | Dimensional and test records | The sample matches the released revision |
| Traceability | Material lots and production logs | Records connect materials to each batch |
| Technical response | Written DFM feedback | Recommendations address existing customer drawings |
| Quoting | Itemized quotation | Tooling and testing costs are stated clearly |
| Intellectual property | China-specific agreement | The correct legal entity accepts suitable protections |
| Production continuity | Work instructions and change records | Volume builds follow the approved process |
| Quality response | Corrective-action procedure | Containment and investigation responsibilities are defined |
As a custom wire harness manufacturer in China, Cloom Tech provides prototype and volume manufacturing under documented production controls. Material availability and testing scope can affect the final schedule. Each quotation should confirm project-specific timing.
Certifications that Matter for Harnesses
IPC/WHMA-A-620 defines wire harness quality and acceptance requirements, while ISO 9001 covers the manufacturer’s quality-management system.
When a custom wire harness manufacturer in China produces automotive assemblies, IATF 16949 adds sector-specific quality requirements. The scope of each certificate must therefore cover the quoted manufacturing site and required work.
IPC/WHMA-A-620
IPC/WHMA-A-620F-2025 is the current industry-consensus standard for cable and wire harness assembly requirements and acceptance. Revision F strengthens guidance on product classification and inspection methodology. Its expanded process-control requirements explain how manufacturers should manage assembly methods and inspection throughout production.
Updated requirements address crimped and soldered terminations. Additional provisions cover protective coverings and testing.
The customer and supplier must agree whether Class 1, Class 2, or Class 3 applies to the assembly. General electronic products fall under Class 1 when the basic function is the primary requirement. Class 2 covers dedicated-service products that require continued performance and extended life. High-performance products use Class 3 when continued operation is required.
Verification should establish the revision and product class stated in the controlled work instructions. Request representative inspection records and confirm that relevant personnel hold current role-specific training. A general “IPC compliant” statement doesn’t show how the factory applies the standard.
ISO 9001
ISO 9001 establishes a general quality-management framework for documented production controls. Its scope can cover purchasing and incoming inspection. Related procedures address calibration and corrective action.
Check the legal entity and factory address shown on the certificate. The stated scope should include the manufacturing of harness or cable assemblies. The certification period should also remain current. A sales office certificate doesn’t establish production controls at another facility.
IATF 16949
IATF 16949 adds automotive quality management requirements when the customer or program requires them. Supporting records may include Production Part Approval Process documentation and process Failure Mode and Effects Analysis. Control plans should connect those requirements to the quoted assembly.
Factory vs. Broker Verification
Verify whether the company named on the quotation operates the factory producing the finished harness. Connecting the quoted business to the production site clarifies who is responsible for meeting its commercial and manufacturing commitments.
Apply the same legal and physical checks to every Chinese wire harness manufacturer, regardless of website quality or marketplace status.
Check The Business License
The Chinese business license identifies the registered entity and its approved business scope. Verify the Unified Social Credit Code, operating status, and registered address through the appropriate official records.
Next, compare the legal name on the quotation and purchase agreement. The invoice and bank beneficiary should show the same entity or a documented relationship. A business license review should confirm that the license’s scope supports the quoted activity.
Inspect The Production Site
An on-site audit provides direct evidence of the operation, while a short-notice live video tour can support initial screening. Ask to see the wire-processing equipment and crimp presses in use. The tour should also cover pull-force equipment and electrical test systems.
Calibration labels should match equipment records. Current work orders can confirm active production, while material identification shows how the site maintains traceability. A broker may provide legitimate coordination when it discloses its role and permits access to the actual factory.
Testing Capability (Crimp Pull Tests, 100% Electrical Testing, Documentation)
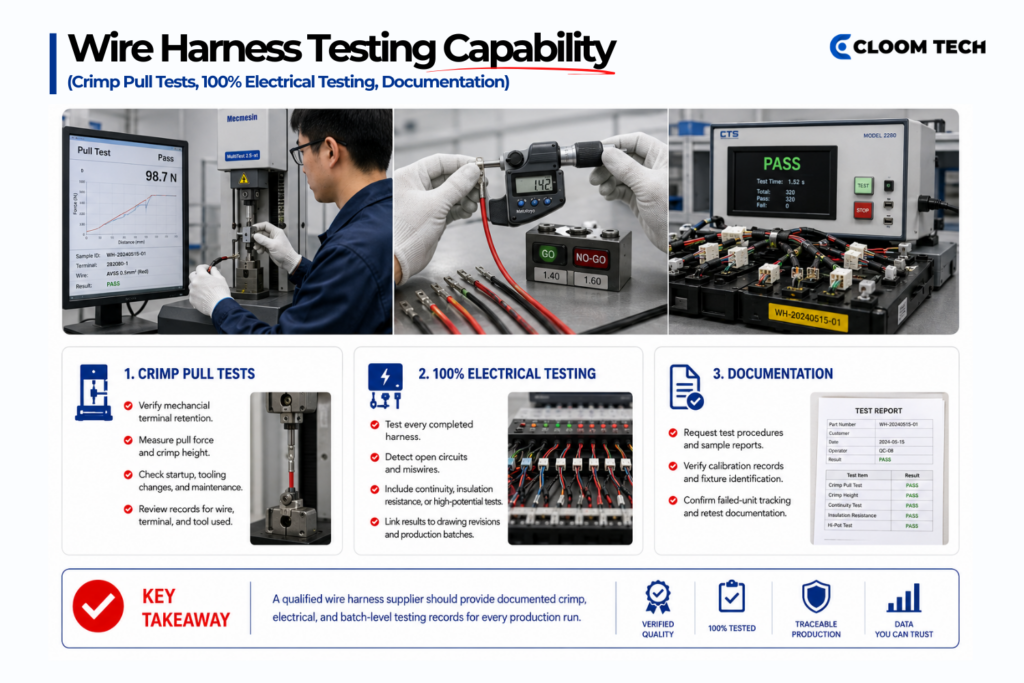
A supplier’s testing capability should verify mechanical connection quality and electrical circuit accuracy through separate methods. Request documented procedures and results linked to each production batch from the wire harness manufacturer in China.
Crimp Pull Tests and Crimp Height
Pull-force testing measures the axial force required to separate a conductor from its terminal. The result confirms mechanical retention, while crimp-height measurement checks the compressed barrel against its specified range.
Request records that identify the wire and terminal combination. The report should state the tool and the measured force. It must also identify the applicable limit. Sampling points should include production startup and tooling changes, with additional checks following maintenance or a failed result.
A pull-force test can pass even if the crimp height falls outside its approved range. Reviewing both measurements provides stronger evidence of process control than visual inspection alone.
100% Electrical Testing
Electrical testing should apply the approved test program to every completed production harness. Fixture-based equipment can detect open circuits and miswires. The specified scope may also include insulation resistance or high-potential testing.
Request a sample report that shows the drawing revision and test limits. Equipment calibration and fixture identification should connect the result to a controlled system. Production records must identify failed units and document retesting after repair.
Cloom Tech provides 100% electrical continuity testing with production quality records. When comparing a custom wire harness manufacturer in China, confirm that its records link each result to the relevant production batch.
Sample and First-Article Evaluation
Sample and first-article evaluation confirms whether the completed harness matches the released drawing and approved materials. Begin by comparing its dimensions and connector orientation with the specification. Then, inspect the quality and verify the crimp and electrical test records before approving production.
Define The Harness Specifications
Before sample production begins, send the supplier the approved drawing and bill of materials with the approved part numbers and wire specifications clearly identified. Along with these documents, include the terminal specifications and test requirements, and state the applicable IPC/WHMA-A-620 class on the drawing.
To maintain this approved baseline, document any permitted deviations and labeling requirements before production begins. Before changing an approved component or process, the supplier must obtain written approval.
Inspect The Physical Assembly
Physical inspection should compare the sample’s dimensions and connector orientation with the released drawing. As part of the same review, check the wire markings and terminal seating, and confirm that the protective materials and strain relief meet the specification.
Once these features align with the drawing, fit the harness within the mating assembly to confirm its routing. If the sample deviates from the approved requirements, these changes must be formally documented and approved through your established engineering change process before proceeding.
Review The Evidence Pack
First Article Inspection (FAI) records should connect the sample to its dimensional measurements and electrical test results. As part of this review, pull-force records should identify the terminals tested, while material certificates confirm the approved components.
To complete traceability, lot records should connect the materials used for the sample to the relevant production batch.
Communication, Engineering Support (DFM Boundary), and Quoting Transparency
Effective communication gives the buyer direct access to people who can resolve production questions and document each approval. Engineering support should clarify how the existing drawing translates into manufacturing requirements without extending into product design. A transparent quotation should then explain the project’s costs and schedule in measurable terms.
Communication and Engineering Support
Communication and engineering support should begin with a named commercial contact who can coordinate with the manufacturing team. When production questions arise, the buyer should have access to personnel who understand the assembly requirements and factory processes.
Written communication should document technical decisions, customer approvals, and schedule changes throughout the project. If a quality issue occurs, a defined escalation path should identify who will coordinate the response.
Design for Manufacturability (DFM) feedback should remain limited to reviewing existing customer drawings. During this review, the manufacturer may identify missing dimensions or incompatible wire and terminal selections. Any material recommendation requires written customer approval before implementation.
Quoting Transparency
A transparent quotation provides a clear cost breakdown, itemizing material and assembly labor. All non-recurring costs, such as tooling and electrical test fixtures, should be listed as separate line items. It should explain how the manufacturer calculated the unit price and identify the requirements included in that price.
To establish an accurate schedule, the quotation should separate material sourcing time from manufacturing time. Sample approval and customer sign-off should appear as distinct schedule dependencies.
IP Protection and NDAs
Protect intellectual property by having the correct Chinese legal entity sign a China-specific non-use, non-disclosure, and non-circumvention agreement before receiving complete drawings or bills of materials. Unlike a standard nondisclosure agreement, these provisions restrict the manufacturer from using, disclosing, or circumventing your IP for their own commercial gain.
China-specific NNN guidance recommends this agreement structure because standard nondisclosure agreements don’t address the full range of manufacturing risks in China. Where production involves related entities or subcontractors, the agreement may need to extend the same obligations to those parties.
The governing law and controlling language should appear in the contract terms. Before transferring the drawings, have a lawyer experienced in Chinese manufacturing agreements adapt the provisions to the transaction.
Red Flags
Red flags include an undisclosed broker relationship, missing testing documentation, and no evidence that the manufacturer applies IPC/WHMA-A-620 requirements.
A disclosed intermediary can remain on a wire harness manufacturer’s shortlist in China when the manufacturing relationship and quality responsibilities are transparent.
Harness-specific concerns include:
- Undefined quality requirements: No IPC/WHMA-A-620 revision or product class is specified.
- Missing crimp evidence: Crimp-height records or pull-force reports aren’t available.
- Unsupported testing claims: Electrical testing procedures or sample results aren’t provided.
- Incomplete first-article records: First articles arrive without measured evidence.
- Uncontrolled material changes: Substitutions lack approval or lot records are missing.
Factory and commercial concerns include:
- Mismatched certification details: Certificates name another entity or production address.
- Unrelated payment accounts: Payment requests name a personal or unrelated account.
- Restricted factory access: The supplier refuses to conduct a factory audit or a live tour.
- Unclear production responsibility: Subcontracting remains hidden, or technical responses lack detail.
- Incomplete pricing: Quoted prices omit tooling or required testing.
How Cloom Tech Measures Up
Cloom Tech documents its manufacturing controls covered by the same checklist applied to every other Chinese wire harness manufacturer.
| Checklist Area | Cloom Tech’s Position |
|---|---|
| Manufacturing footprint | Production in China and the Philippines |
| Product model | Custom manufacturing from customer specifications |
| Workmanship | IPC/WHMA-A-620 processes |
| Quality systems | ISO 9001, TS16949 and IATF 16949 |
| Materials | Global sourcing of approved harness components |
| Inspection | Internal controls with third-party inspection options |
| Testing | 100% electrical continuity testing with production quality records |
| Technical boundary | DFM feedback on pre-existing customer drawings |
| Prototype timing | Approximately 2–3 weeks, depending on requirements |
| Production timing | Approximately 4–5 weeks after approval |
| Track record | Work associated with Honda, Honeywell, Mahle, and GEELY |
Send Cloom Tech your pre-existing drawings and bill of materials, along with your expected volumes and testing requirements. Based on this information, our team can provide Design for Manufacturability (DFM) feedback on those drawings and prepare transparent pricing for prototype and volume manufacturing.
Contact us to discuss your requirements with the China-based custom wire harness manufacturer team and request a project-specific quote.
How to Evaluate a Chinese Wire Harness Manufacturer FAQs
What is the difference between a prototype and a first article?
A prototype is used to check whether the proposed design fits and functions as intended before the manufacturing specification is finalized. A first article verifies that the released design can be produced through the intended manufacturing process. Its inspection records document the measured results before volume production begins.
When does a harness require insulation-resistance or high-potential testing?
Insulation-resistance or high-potential testing applies when the released specification requires verification beyond continuity and miswire checks. The decision depends on the operating voltage and insulation requirements. Before testing begins, the customer should approve the method and limits based on the harness application.
What happens when a crimp pull-force result fails?
A failed pull-force result requires the manufacturer to stop the affected crimping operation and identify all assemblies produced since the last passing check. After investigating the terminal, wire, and tooling setup, the manufacturer should correct the cause and repeat the test. Production can resume once the crimp meets the approved limit and the result is documented.
Can a manufacturer change an approved component after sample approval?
A manufacturer should only change an approved component after receiving written customer authorization. Before approving, the customer should review how the proposed substitute affects fit and electrical performance. The drawing and bill of materials must then reflect the authorized component.
Which production changes require another First Article Inspection?
A design revision or material substitution may require another First Article Inspection (FAI) when the change could affect the approved harness. Changes to tooling, manufacturing processes, or production location may trigger the same requirement.
The customer’s quality agreement should specify when a complete or partial FAI is required. SAE AS9102C establishes formal FAI documentation requirements for aerospace programs.
Can production move to another factory after approval?
Production should move to another factory only after written customer approval and qualification of the proposed site. The review should confirm that the new operation can follow the released specifications and approved test requirements. A new First Article Inspection may be required before volume manufacturing resumes.
Back to Top: How to Evaluate a Chinese Wire Harness Manufacturer: A Buyer’s Vetting Checklist
